Пищевая ПЭТ-смола, идеальное сырье для бутылок для напитков и упаковочных контейнеров для пищевых продуктов
2026-09-14 08:56:24
Food and beverage packaging production demands an optimal balance of hygienic safety, long-term shelf-life stability, aesthetic presentation and cost-efficient mass manufacturability. Among all thermoplastic packaging substrates, food grade PET resin stands out as the most universally recognized qualified raw material, strictly compliant with global food contact regulations. Unlike industrial-grade PET and modified plastic alternatives, professionally formulated food grade PET features pure molecular composition, zero harmful precipitation and precise gas barrier performance. It addresses the core industry pain points of food oxidation, beverage flavor attenuation, packaging safety risks and high manufacturing costs, becoming the exclusive mainstream material for bottled beverages, sealed food containers and disposable food packaging solutions worldwide.
Core Qualification & Safety Advantages of Standard Food Grade PET Resin
The fundamental competitiveness of food grade PET lies in its rigorous food-contact safety certification system and ultra-pure material characteristics. Premium food grade PET is produced from virgin polymerization raw materials without recycled impurity mixing, eliminating residual heavy metals, volatile organic compounds and harmful plastic additives that often appear in generic plastic resins. It fully complies with FDA food contact regulations, EU LFGB standards and global food safety testing specifications, supporting long-term safe contact with acidic beverages, oily food, neutral drinking water and low-temperature preserved food.
Different from modified PP and PS materials that rely on auxiliary additives to meet food-grade standards, pure PET resin achieves inherent hygienic safety through molecular structural stability. It does not release chemical precipitates or produce odor contamination during normal storage and use, avoiding food deterioration and safety incidents caused by packaging material migration. This inherent safety makes it the preferred material for high-standard food and beverage packaging that requires full-cycle hygienic control from production to terminal consumption.
Superior Gas Barrier Performance Extends Food & Beverage Shelf Life
Shelf life stability is the core indicator that determines food packaging practicability, and food grade PET possesses unparalleled gas and moisture barrier advantages over other commodity plastics. Its compact molecular structure effectively blocks external oxygen infiltration and internal gas escape, solving two key deterioration problems in food and beverage storage: oxidative spoilage of food contents and carbon dioxide loss of carbonated drinks.
For carbonated beverages, soda water and sparkling drinks, food grade PET locks internal CO₂ to maintain stable taste and bubble activity, avoiding flat flavor caused by long-term gas leakage. For fruit juices, tea drinks and packaged snacks, its excellent oxygen barrier performance slows down ingredient oxidation, color fading and nutrient loss, greatly extending commercial shelf life. In addition, its stable moisture-proof property prevents dry food from absorbing moisture and caking, ensuring consistent taste and product quality throughout circulation and sales.
Balanced Mechanical & Aesthetic Properties for Terminal Sales Presentation
Modern food and beverage packaging not only undertakes protection functions but also serves as core product display carriers. Food grade PET resin features crystal-clear transparency and high surface gloss, presenting the original color and texture of beverages and food intuitively. Compared with opaque HDPE and low-transparency modified plastics, PET’s high visual permeability significantly improves product shelf appeal and consumer purchase willingness, bringing implicit brand value for food and beverage enterprises.
While maintaining high appearance quality, food grade PET delivers excellent structural toughness and shatter resistance. It avoids the fragile defects of glass packaging and the soft deformation problems of ordinary plastic packaging. Lightweight and high-strength characteristics reduce breakage loss during transportation and sales, and its stable structural rigidity supports diversified hollow molding, covering personalized bottle body shapes, irregular container structures and portable thin-wall packaging designs to meet differentiated market packaging demands.
Excellent Processing Adaptability for High-Volume Industrial Production
Food and beverage packaging belongs to typical high-volume standardized manufacturing scenarios, requiring raw materials to adapt to high-speed continuous molding and stable batch consistency. Food grade PET resin has uniform molecular weight distribution, stable melt fluidity and moderate molding temperature window, perfectly matching high-speed bottle blowing, injection molding and stretch molding processes.
During continuous mass production, food grade PET maintains stable viscosity and molding consistency, effectively reducing defective rates such as bottle body uneven thickness, bubble spots and molding deformation. Its low shrinkage characteristics ensure high dimensional accuracy of finished bottles and containers, supporting automated assembly, filling and sealing line matching. Excellent processing performance greatly improves production line efficiency and reduces unit manufacturing costs for packaging factories, realizing high-yield and low-loss industrial production.
Temperature & Environmental Adaptability for Diverse Storage Scenarios
Commercial food and beverage products face variable storage and transportation environments including normal temperature placement, low-temperature refrigeration and cross-regional temperature changes. Food grade PET has wide temperature adaptability, maintaining stable structural and chemical performance in the temperature range of -20°C to 60°C. It will not become brittle and crack in low-temperature refrigeration environments, nor produce soft deformation and molecular aging under normal temperature long-term placement.
In addition, food grade PET features outstanding chemical inertness, resisting corrosion from beverage acidity, fruit acid and food oil stains. It does not react with internal food ingredients or external environmental pollutants, ensuring zero secondary pollution during product circulation. This stable environmental adaptability guarantees packaging safety in complex commercial logistics and terminal sales scenarios.
Sustainable & Cost-Effective Long-Term Industrial Value
In terms of comprehensive industrial cost, food grade PET achieves a perfect balance of safety, performance and economy. Although it meets top-tier food safety standards, its raw material and molding costs are far lower than glass, stainless steel and high-end engineering packaging materials. The lightweight feature greatly reduces transportation weight and logistics costs for beverage and food enterprises, bringing substantial long-term cost savings in large-scale circulation.
Meanwhile, food grade PET is highly recyclable with stable renewable performance, complying with global low-carbon packaging and sustainable development policies. It supports brand ESG assessment and green product certification, helping food and beverage enterprises enhance market competitiveness and meet increasingly stringent environmental packaging requirements.
Typical Industrial Application Scenarios
Relying on multi-dimensional performance advantages, food grade PET resin covers almost all mainstream food and beverage packaging fields:
-
Beverage bottle packaging: Pure water bottles, carbonated drink bottles, fruit juice bottles, tea beverage bottles and functional drink containers
-
Sealed food containers: Transparent fresh-keeping boxes, sealed snack cans, condiment packaging bottles and honey storage containers
-
Disposable food packaging: Transparent lunch boxes, food packaging trays and portable food storage packaging
-
Special food packaging: Low-temperature refrigerated food packaging and vacuum-sealed food containers requiring long-term fresh preservation
Conclusion
Food grade PET resin has become the ideal core raw material for beverage bottles and food packaging containers by virtue of inherent food safety, superior gas barrier fresh-keeping performance, high appearance texture, stable processing adaptability and sustainable cost advantages. It solves the multiple industry pain points of food safety risks, short shelf life, unstable molding quality and high circulation costs existing in traditional packaging materials. For modern food and beverage manufacturing and packaging enterprises, selecting standardized food grade PET resin is the most reliable and cost-effective material solution to ensure product safety, optimize market display effects and realize large-scale sustainable production.




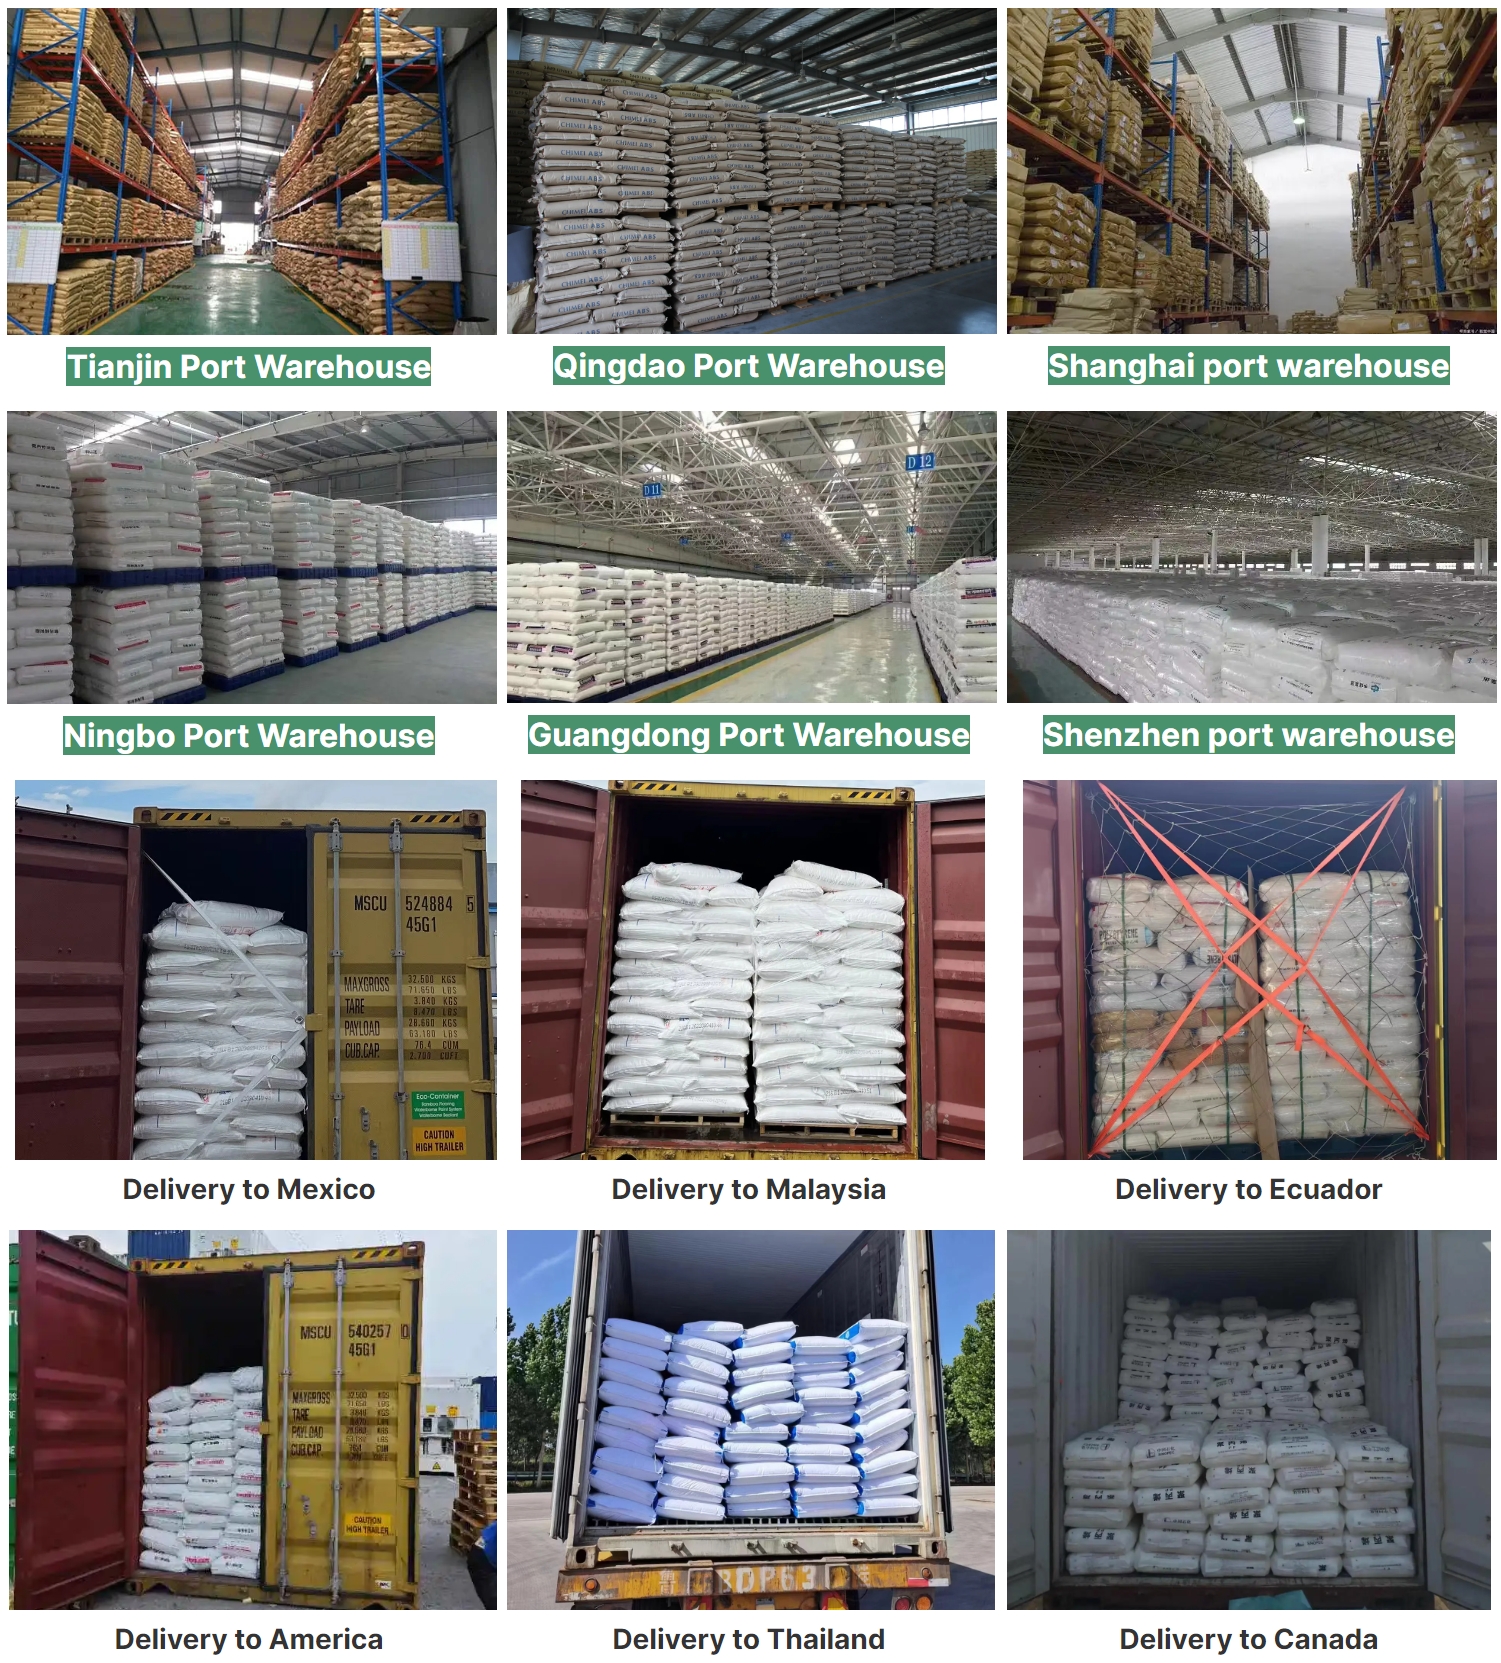
We have established long-term cooperative relations with more than 60+ well-known enterprises all over the world

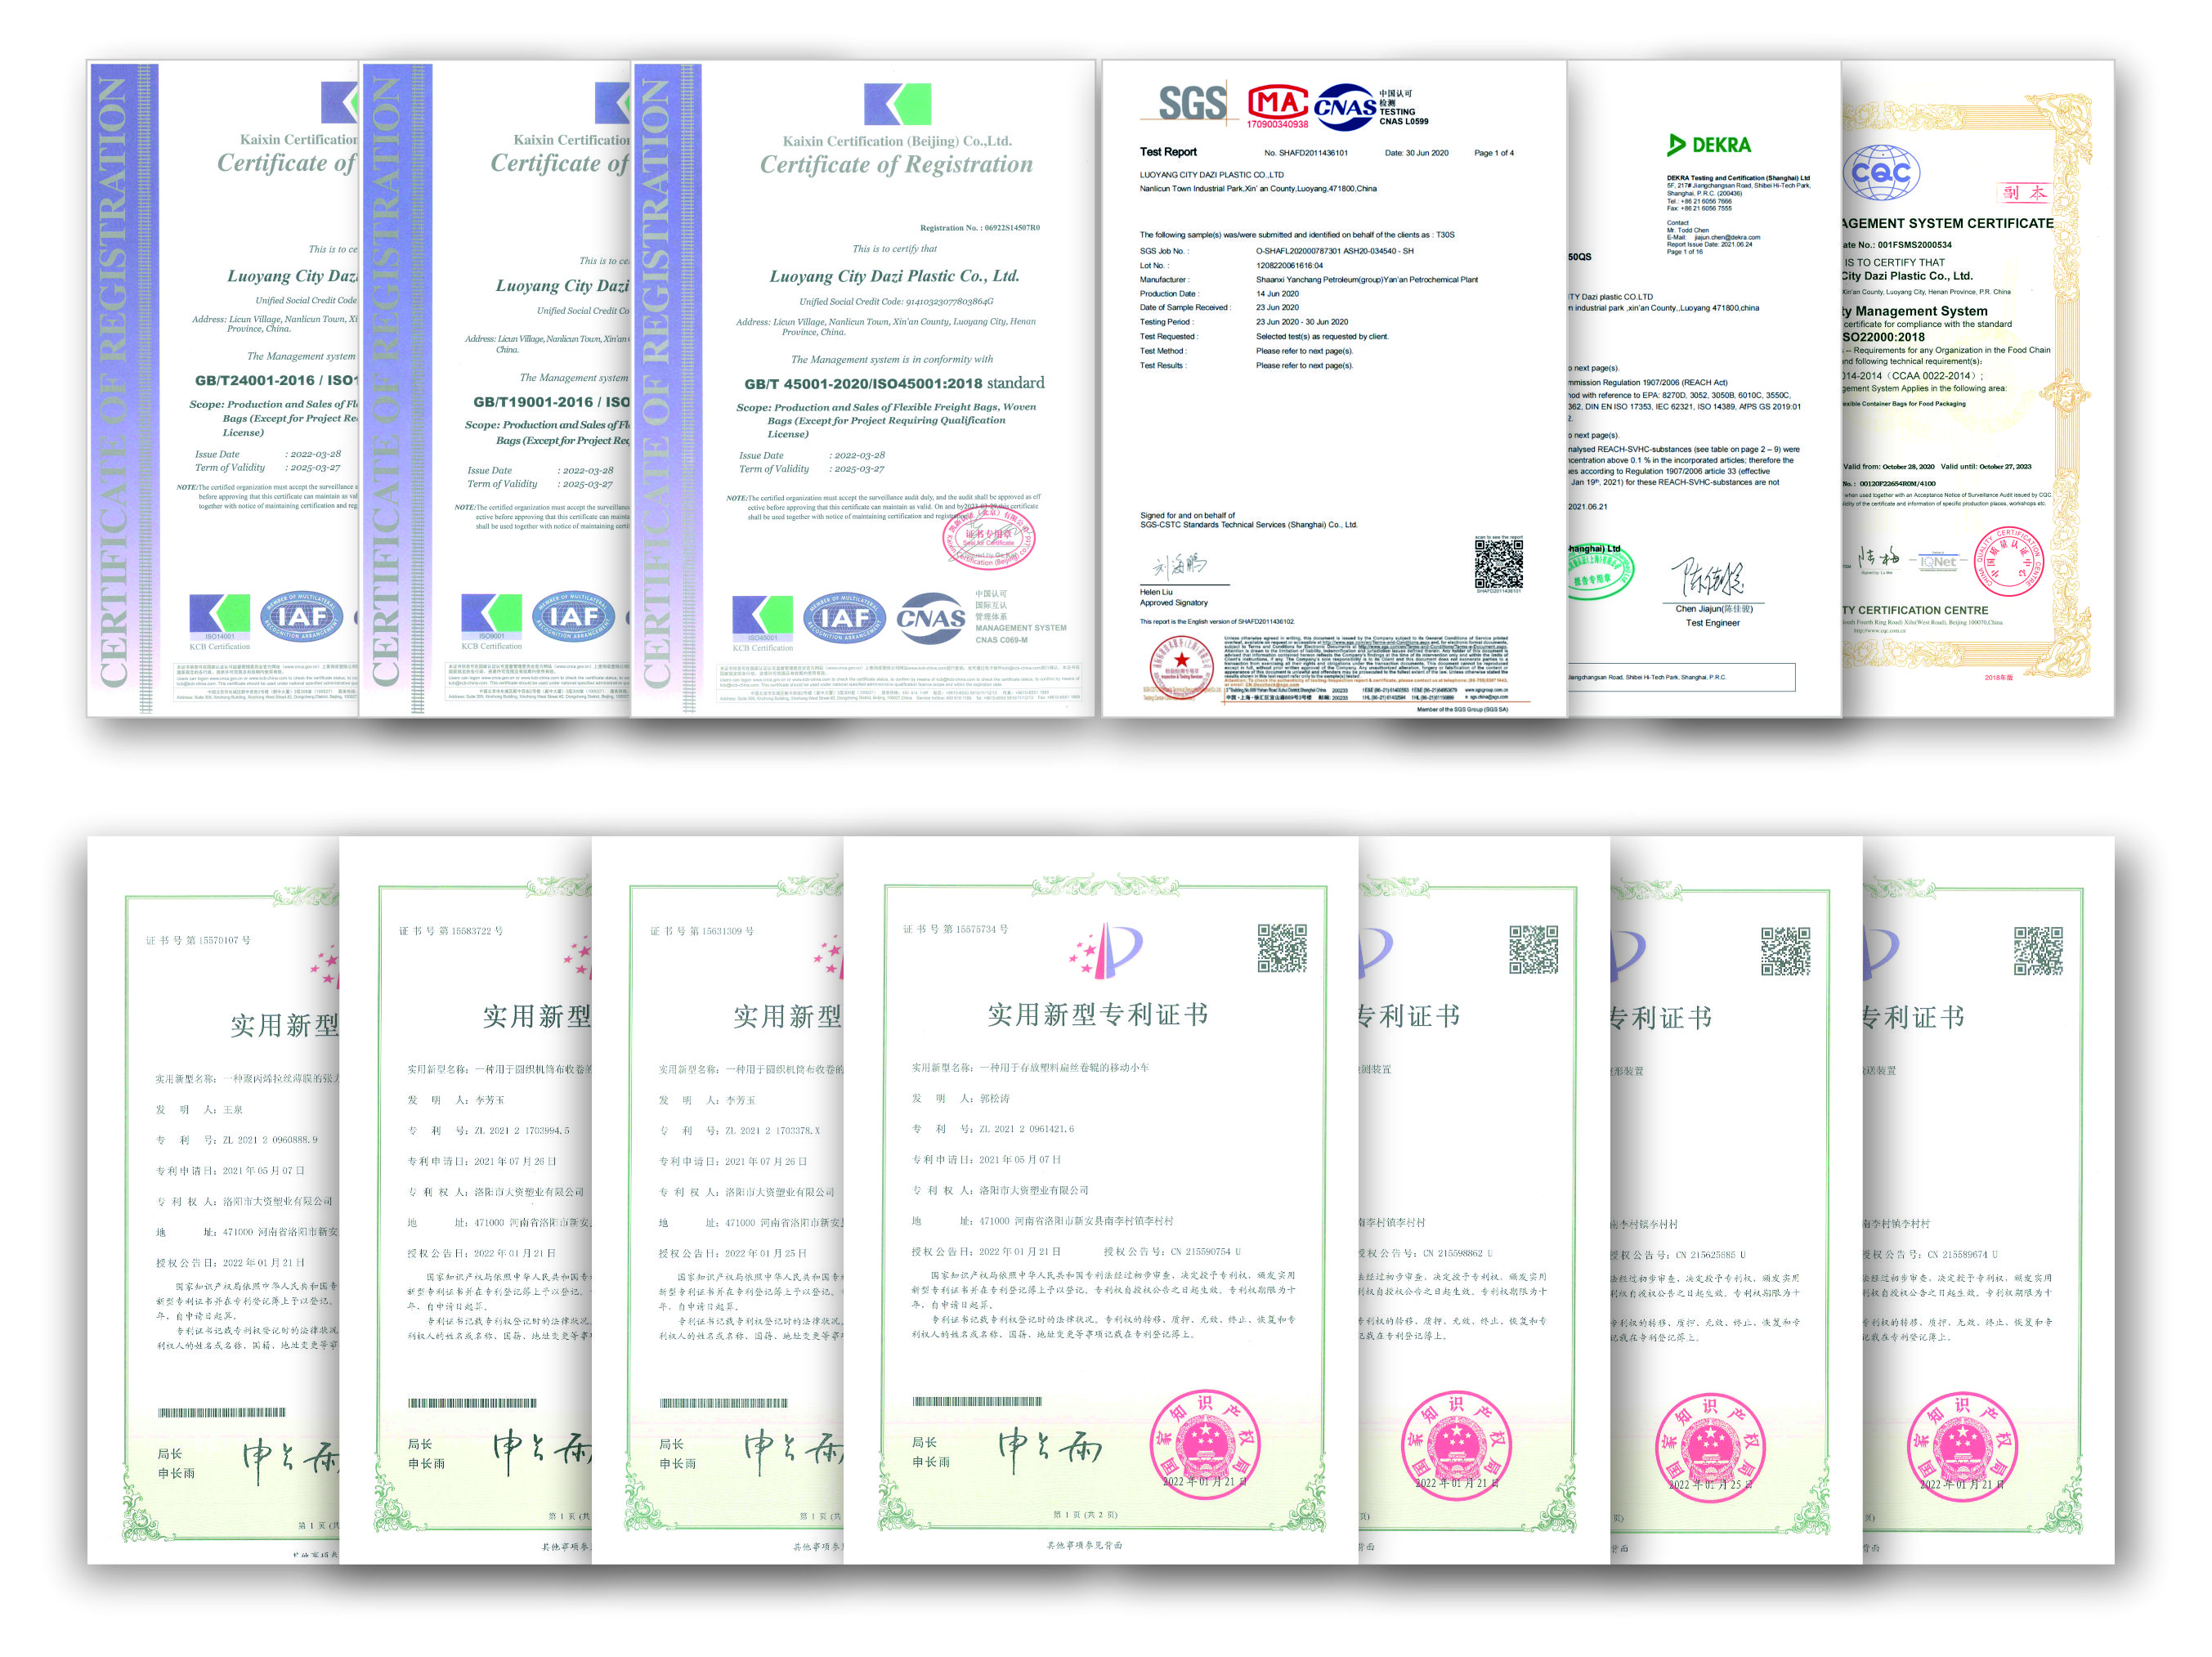
Our company has 12 certifications and 57+ patents.
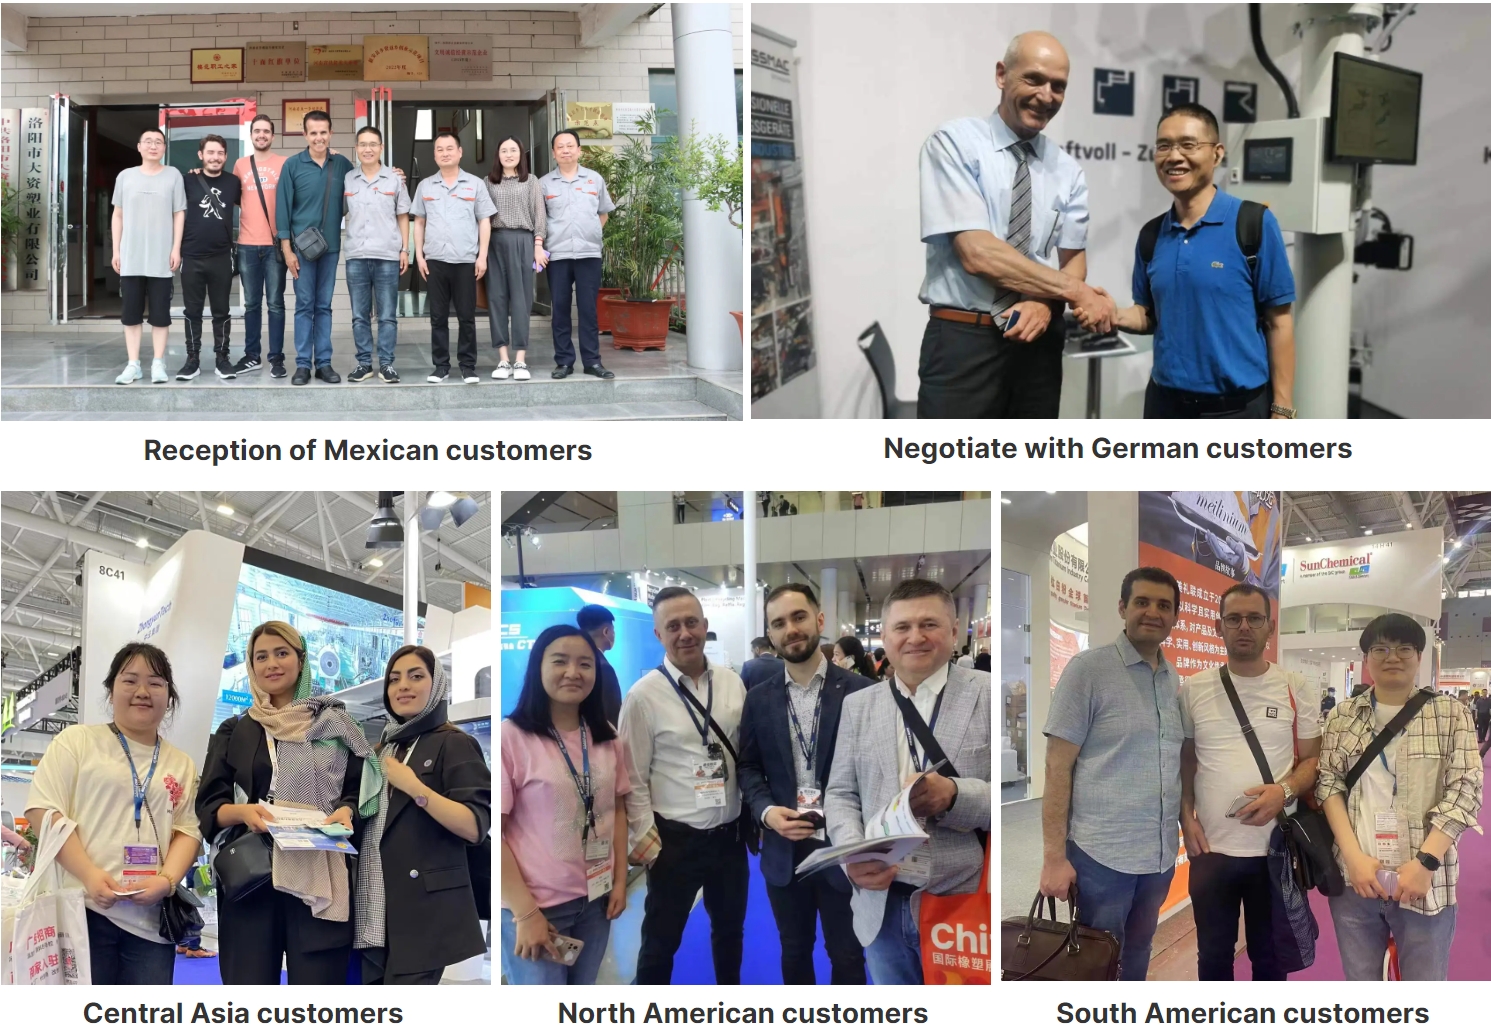

23 years' experience Professional purchasing consultant with a supply chain of 1200+ plastic raw materials in China.